
Six processes in one line
Integrate loading, perforation, notching, beveling, cutting and unloading around one programmed structural-steel workflow.

Bodor U10 Pro | Automatic structural steel processing
A fully automated laser production line developed for H-beams and I-beams. U10 Pro combines loading, perforation, notching, beveling, cutting and unloading in one connected process, with UK specification, installation, training and long-term support from World Machinery.
Profile size, length, weight, laser power, loading, bevel capability, Tekla workflow and site requirements depend on the selected configuration. Confirm all details in a current written World Machinery quotation.

Six processes | automatic operation | higher throughput
The U10 Pro concept brings the main H-beam preparation stages together so material can move from stock loading through hole cutting, notch forming, bevel preparation, profile separation and sorted unloading without being transferred between several independent machines.
Integrate loading, perforation, notching, beveling, cutting and unloading around one programmed structural-steel workflow.

Automatic loading and length-based unloading are intended to reduce routine handling and secondary material distribution.

A connected process can reduce waiting between operations and shorten the route from structural drawing to finished component.
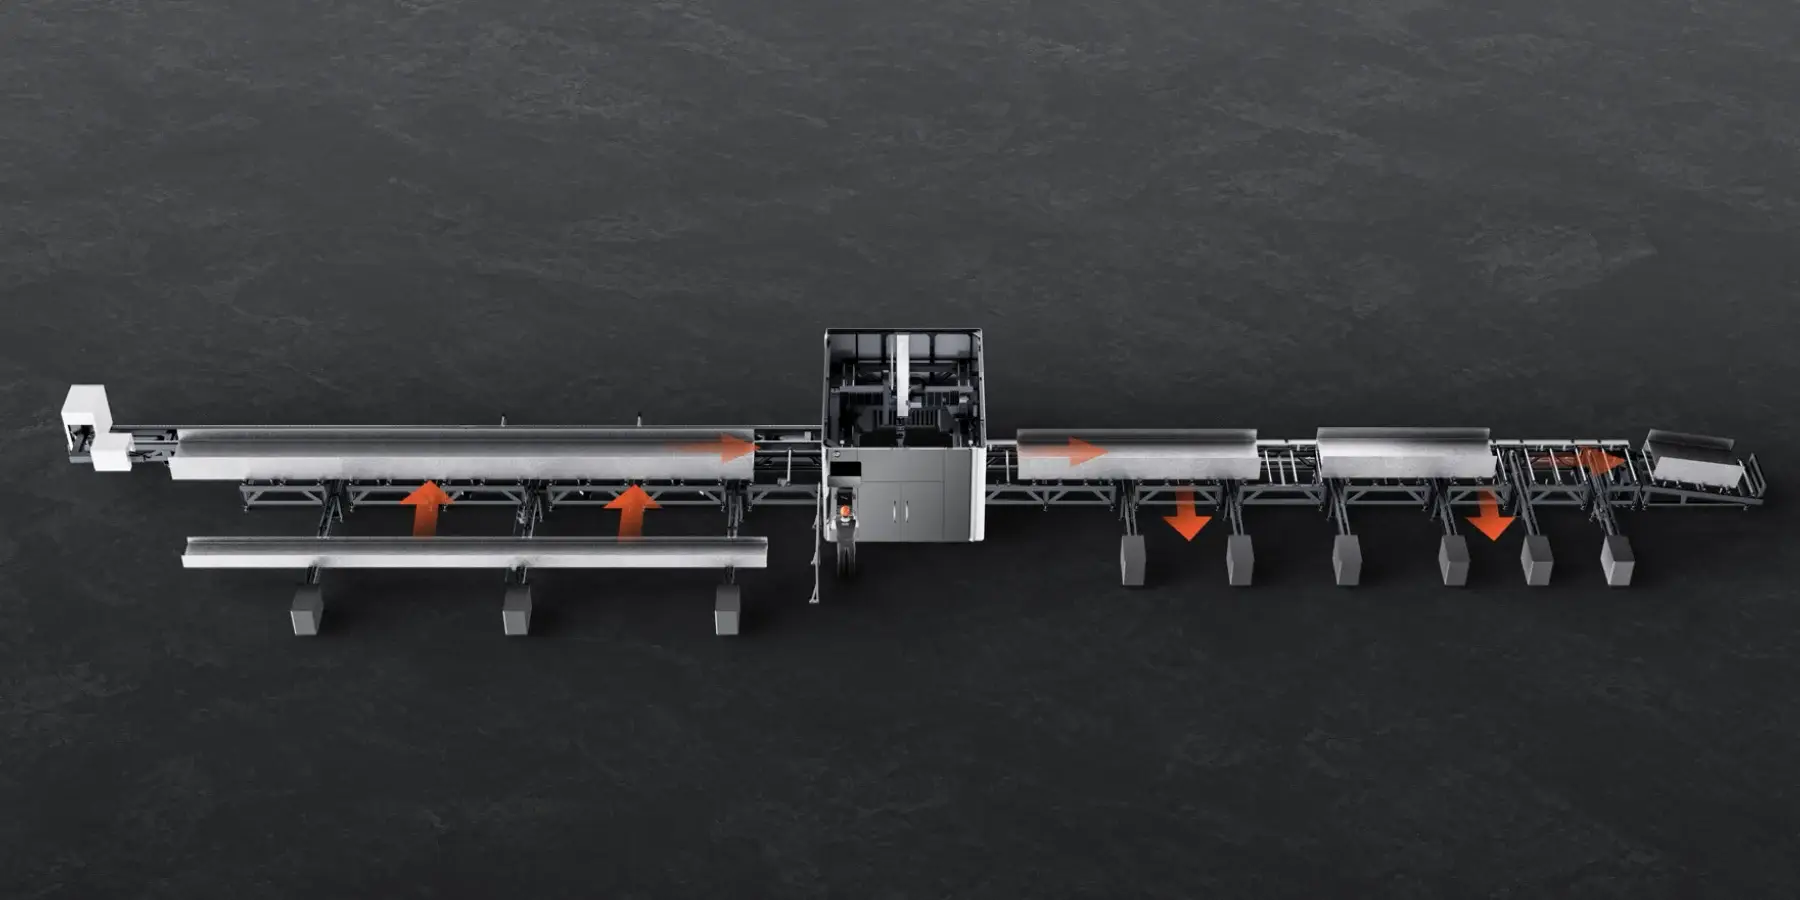
Fully automatic operation
Bodor describes the U10 Pro as an automatic line from the transition area through processing and unloading. The loading process is published as completing in under 20 seconds for suitable stock, while finished workpieces can be sorted according to length.
Introduce suitable structural profiles to the line without routine manual placement during the prepared production cycle.
Move the profile from the transition area into the cutting zone and complete the programmed operations in sequence.
Sort completed workpieces by length to reduce secondary material distribution after cutting.
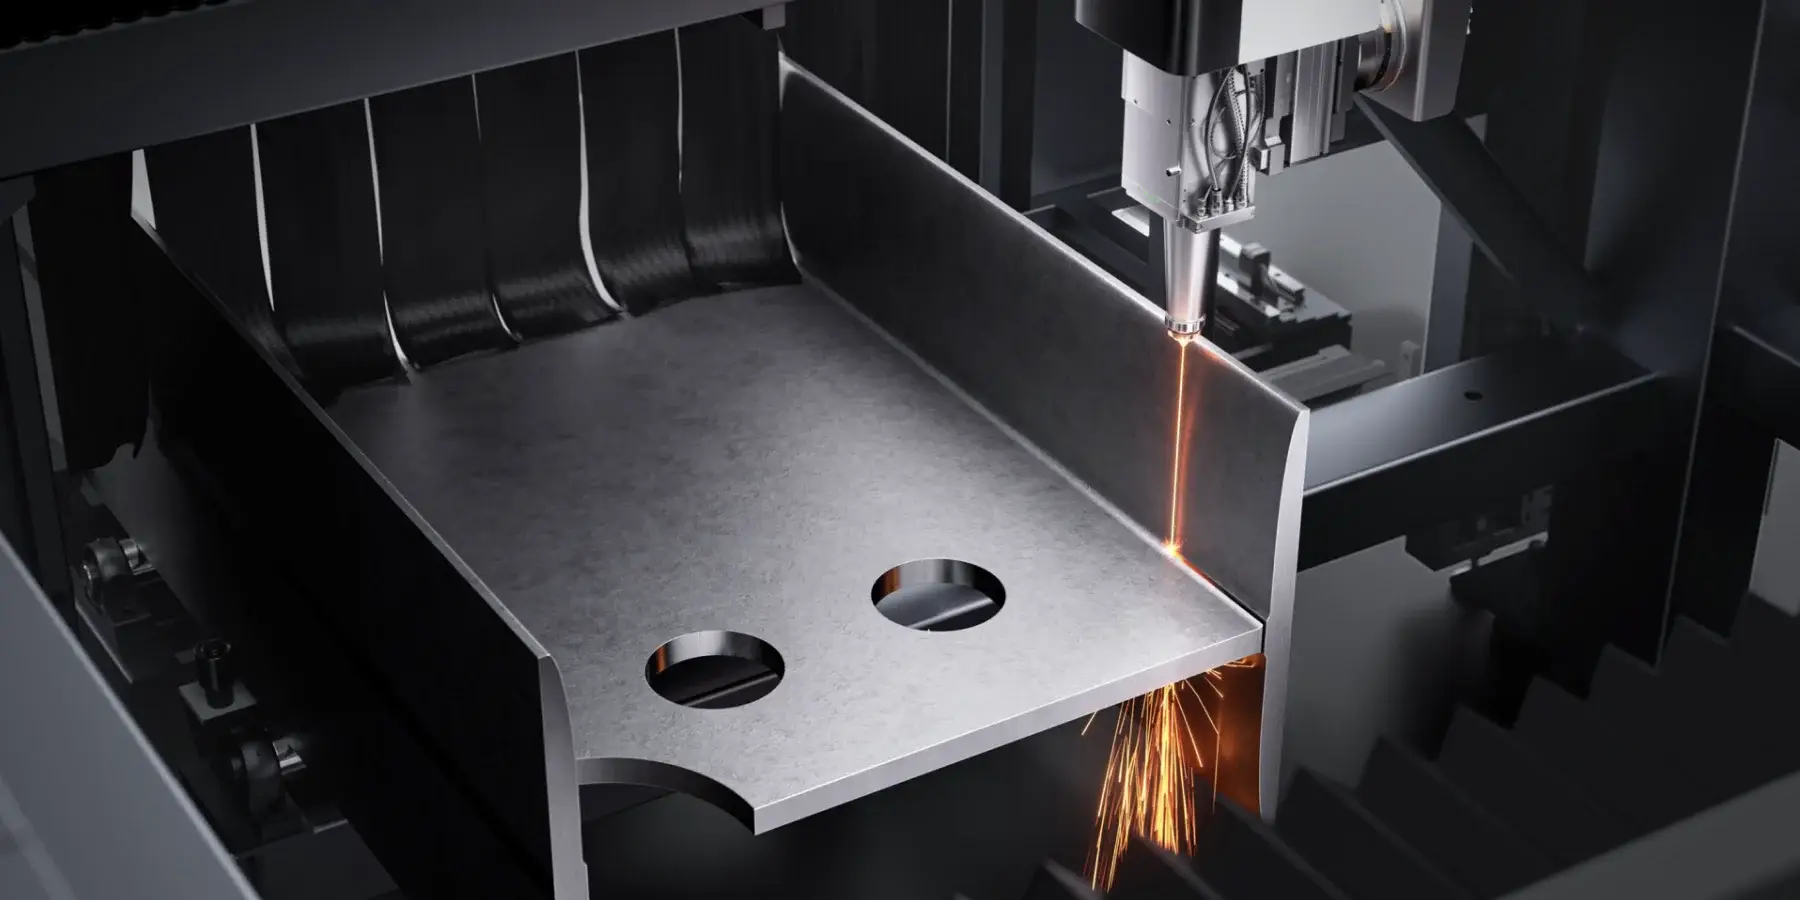
One-step notch forming
The U10 Pro cutting head maintains a controlled stand-off above the workpiece while forming the notch. Bodor presents the process as eliminating manual secondary polishing and doubling notch-processing efficiency for suitable applications.
Create the structural connection feature without moving the profile to a separate manual preparation stage.
The process is intended to reduce or remove manual polishing where the required edge condition can be achieved by laser.
Representative drawings and steel sections should be tested because access, thickness, geometry and weld requirements influence the result.
Five-axis linked cutting
Bodor describes a 180-degree reciprocating cutting head with five-axis linkage across A, C, X, Y and Z. The configuration is intended to improve access to structural-steel surfaces and support optional bevel cutting while reducing repeated repositioning.
Published motion and efficiency claims are manufacturer references. Actual cutting access, tolerance, finish and cycle time depend on profile geometry, material, thickness, fixtures, programming and the supplied machine configuration.

Digital workflow and connected production
The benefit of U10 Pro depends on how drawings, stock, loading, cutting and finished-part handling are connected. World Machinery can review the customer’s detailing and production workflow before the final configuration is agreed.
 Drawing workflow
Import compatible 3D structural models, ungroup components and generate processing codes for the following operations, subject to the confirmed software and licence workflow.
Integrated lineBring the main profile-preparation stages together to reduce transfers between separate machines and manual workstations.
Automatic handlingCoordinate material entry, programmed cutting and length-based unloading as one production line rather than independent steps.
Connection detailsUse laser cutting to form suitable locking notches in one pass and reduce later manual preparation where the application permits.
Published configuration and technical references
The original World Machinery page includes a technical-parameters image. The redesign retains that graphic and adds a plain-language summary of the manufacturer-published ranges, while making clear that the final delivered specification must be confirmed in writing.

Bodor publishes I-beam and H-beam processing, a 600 × 300mm to 1000 × 600mm profile-size range, maximum profile length from 6200mm to 13,500mm and a maximum profile-weight reference of 6 tonnes.
Plan the machine, loading area, transition section, processing zone and unloading arrangement as one structural-steel production cell.
Confirm the supplied cutting head, bevel capability, supported angles, material range, tolerances and required finished edge through representative trials.
Confirm the Tekla version, file responsibility, licences, ungrouping method, code-generation process and approval workflow before installation.
Specify around real structural-steel production
A reliable proposal starts with representative profiles, drawings, planned operations and site information. World Machinery can then confirm the suitable line length, cutting package, automation, software, extraction and handling arrangement.
List I-beams, H-beams and any other sections together with the normal and maximum width, height, flange and web thickness.
Confirm incoming stock length, maximum profile weight, bundle or single-piece loading method and the required finished-part length range.
Provide representative drawings showing perforation, locking notches, end cuts, markings, bevels and downstream welding requirements.
Plan line footprint, lifting, stock entry, sorted unloading, extraction, services, Tekla data, programming responsibility and service access.
World Machinery UK support
World Machinery can support application review, Tekla workflow discussions, sample processing, factory-layout planning, installation, commissioning, operator training, planned maintenance and qualifying finance options for the complete U10 Pro project.
Review structural sections, connection details, lengths, weights, material grades, bevels and required edge conditions.
Use real steel sections and production drawings to assess notch quality, five-axis access, bevel preparation and cycle assumptions.
Coordinate access, foundations, power, gas, extraction, loading, unloading, commissioning and practical handover.
Protect uptime with UK technical support and discuss finance routes for qualifying machinery projects.
U10 Pro questions
Final answers depend on the supplied line length, profile range, loading arrangement, cutting head, software, material and optional equipment. World Machinery can provide a current written configuration for the project.
The U10 Pro is designed primarily for automated H-beam and I-beam structural-steel processing. It integrates loading, perforation, notching, beveling, cutting and unloading in one production line.
Bodor publishes a profile-size range from 600 × 300mm to 1000 × 600mm. Section shape, flange and web thickness, straightness, weight and specific feature access must still be reviewed for the application.
The current manufacturer information publishes maximum profile lengths from 6200mm to 13,500mm, a maximum profile-weight reference of 6 tonnes, and automatic-loading workpiece lengths from 1500mm to 13,500mm. Confirm the selected line configuration in writing.
Bodor publishes a reference of under 20 seconds for suitable profile loading. Actual time depends on profile dimensions, weight, orientation, loading method and the complete line configuration.
Bodor describes one-step notch forming that can reduce or eliminate later manual polishing for suitable connection details. Representative sections should be tested because geometry, thickness and required edge condition affect the result.
Bodor describes 180-degree reciprocating motion and five-axis linkage across A, C, X, Y and Z, with bevel cutting available. The supplied head, bevel range, material limits and tolerances must be confirmed for the machine offered.
The manufacturer describes compatibility with Tekla drawings, rapid component ungrouping and automatic generation of processing codes. Confirm the Tekla version, licences, supported file formats and programming responsibilities before ordering.
World Machinery can support application review, factory planning, representative trials, installation, commissioning, operator training and ongoing UK service for the agreed project scope.
Plan your U10 Pro project
Share representative profiles, drawings, connection details, lengths, weights, material grades, annual volume, Tekla workflow and factory layout. The team can then identify the correct configuration and next steps.
Unit 5 Alveley Industrial Estate
Alveley, Bridgnorth, Shropshire WV15 6HG
Provide the main profile, processing and site details below and World Machinery will contact you about the next step.